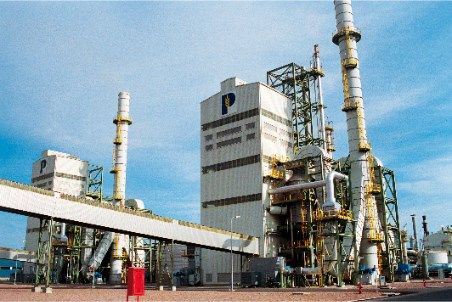
The order marks the first commercial application of PARSYN®, a compressor train concept developed by Everllence for the production of green ammonia. AM Green is converting its existing natural gas-based ammonia and urea production complex into a green ammonia production facility. The Everllence compressor train will serve one of the plant’s production units, designed to produce 1500 tpd of green ammonia, or approximately 525 000 tpy. This production capacity is expected to avoid around 1 Mt of CO2 emissions annually compared with conventional ammonia production. Phase 1 of the Kakinada project will have a green ammonia production capacity of 1 Mtpy.
The project is intended to supply international markets. AM Green has signed a long-term agreement with Uniper in Germany for the purchase of up to 500 000 tpy of renewable ammonia from its projects, with first shipments from Kakinada expected as early as 2028. In addition, AM Green was selected as the sole winner of the Asian lot in the H2Global auction run by HINT.CO GmbH (Hintco). The award secures a long-term purchase agreement to supply Germany with renewable fuels of non-biological origin (RFNBO) ammonia from Phase 2 of the Kakinada project, with first deliveries expected in 2029.
Sunil Sharma, Sales Manager India at Everllence, said: “The Kakinada project is a significant step towards producing green ammonia at industrial scale in India. By converting existing facilities to use renewable hydrogen, AM Green is showing how established industrial infrastructure can become part of a lower-carbon production chain. We are pleased that our first PARSYN® compressor train will contribute to this project.”
Ammonia is produced by combining hydrogen and nitrogen under high pressure. A synthesis gas compressor raises the pressure of this gas mixture before it enters the ammonia synthesis loop. In conventional plants, the compressor is typically driven by a steam turbine, largely using steam generated during the production of hydrogen from natural gas. Green ammonia production generates much less process steam. The PARSYN® train supplied for Kakinada therefore uses an electric motor as its drive.
PARSYN® — short for parallel syngas compressor — arranges two compressors in parallel and connects them through a gearbox. This allows each compressor to operate at a suitable speed while making the train more compact and improving access for maintenance.
Markus Schürmann, Senior Sales and Development Manager Green Ammonia at Everllence, commented: “PARSYN® is about more than choosing the right compressors. We looked at the entire train and how its components work together in a green ammonia plant. The concept is new for ammonia plants, but it builds on decades of experience in designing compressors and machinery trains for demanding industrial processes. By arranging two compressors in parallel and matching each to its operating requirements, we can make the train more compact and improve its efficiency. That helps reduce both the investment needed to build the plant and the energy required to run it.”
Everllence will supply two barrel-type RB compressors with an electric motor, gearbox, dry gas sealing system, coolers, lubrication system, controls, and instrumentation. The scope also includes performance testing, dynamic simulation, and process piping engineering.
Everllence’s process gas compressor experts in Oberhausen, Germany, developed the PARSYN® concept and the overall train. The RB compressors will be manufactured and performance tested in Zurich, Switzerland, while packaging and integration will take place in Oberhausen. Delivery is scheduled for late 2027, with commissioning planned for 2028.